7 Tips for Choosing the Best Conveyor Scale
Choosing the right Conveyor Scale is not just a matter of comparing prices or reading accuracy claims. The right unit must suit your material, belt speed, production rate, and operating environment. A fine, dusty product behaves differently from damp aggregate. Even a small change in belt tension can affect readings. Small details matter.
For this guide, a fictional composite specialist, conveyor-weighing engineer Alex Morgan, offers this original reminder: “A scale earns trust through repeatable readings under real operating conditions.” Morgan is an illustrative character, not a real expert or source of a published quotation. That distinction matters; equipment decisions deserve evidence, not invented credentials. The seven tips ahead focus on practical checks: capacity, accuracy needs, belt and material characteristics, installation, calibration, system integration, and ongoing support. They can help buyers ask sharper questions and compare options on more than a brochure’s headline specifications. Still, no checklist replaces a site assessment. Dust, vibration, changing loads, and uneven maintenance can complicate even a well-chosen system. There is no perfect setup. The goal is a Conveyor Scale that fits the process, produces dependable data, and can be maintained by the people who use it.
Understanding How Conveyor Scales Measure Material Flow
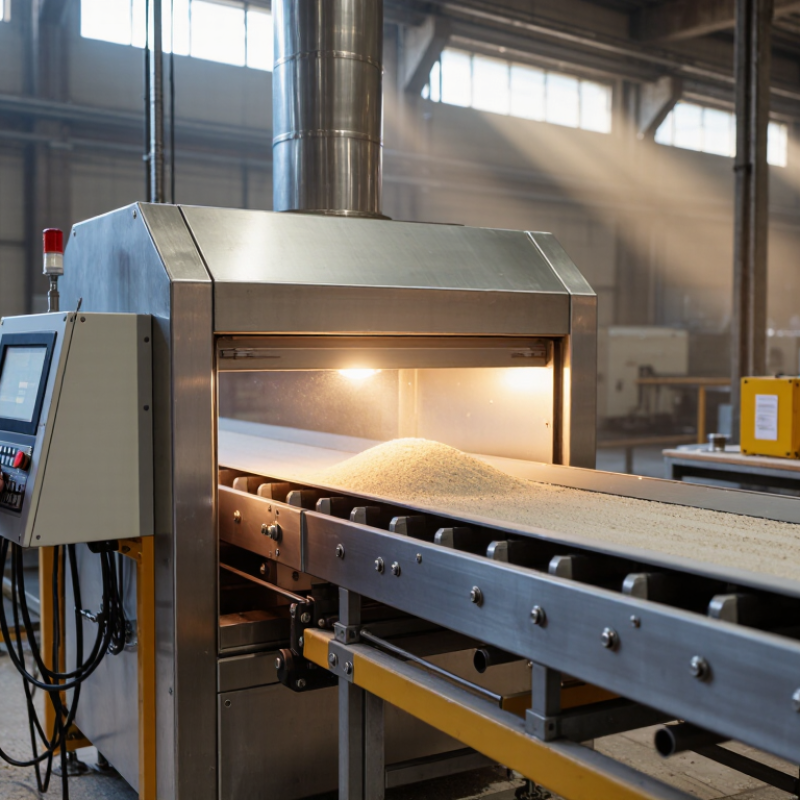
A conveyor scale estimates mass flow by combining the material’s weight on a short belt section with belt speed. Load cells beneath the weigh idler detect the force from material passing over it. A speed sensor tracks belt movement, while an integrator combines both signals into a flow rate, often expressed in tonnes per hour. More material on the belt, or a faster belt, raises the calculated rate. That sounds simple. Dust, vibration, uneven loading, and belt tension can still distort readings.
NIST Handbook 44 lists belt-conveyor scale accuracy classes including 0.25%, 0.5%, and 1.0%. These figures are useful reference points, not automatic guarantees for a working conveyor. A scale’s result depends on installation, calibration, and operating conditions. For example, material arriving in a lopsided stream may load one side of the belt and affect the measurement. Regular checks using known test loads or material tests can reveal drift. In practice, a scale may look stable while slowly diverging from actual throughput; that deserves attention, even when production figures seem plausible.
Defining Your Material and Throughput Requirements
Define the material before comparing conveyor scales. Is it dry sand, damp ore, grain, or recycled aggregate? Particle size, bulk density, moisture, abrasiveness, and stickiness all affect belt loading. Wet lumps may surge; fine powder can cling to the belt. Small details matter.
Then measure real throughput, not just the nameplate rate. Record typical, peak, and minimum flow in tons per hour, including shift hours and batch surges. The USGS Mineral Commodity Summaries 2024 reports U.S. crushed-stone production of about 1.5 billion tons in 2023, a reminder of the scale of bulk-material handling. That national figure cannot size your scale. Site measurements must. Convert daily tonnage into hourly demand and allow for brief peaks without exceeding the scale’s rated belt loading. A single average can be misleading—and easy to over-trust.
Check that expected loads stay within the scale’s calibrated operating range at both low and high flow. NIST Handbook 44, Section 2.21, specifies requirements for belt-conveyor scale systems; consult its applicable test and tolerance provisions when measurements support commercial transactions. CEMA’s Belt Conveyors for Bulk Materials offers further design context for belt and material conditions. Keep a simple log of flow readings, moisture, and interruptions. It may expose a mismatch that a specification sheet misses.
Comparing Scale Capacity, Accuracy, and Technology
Choosing a conveyor scale starts with the material, not the catalog. Compare rated capacity with peak throughput, belt speed, and sudden surges from the feeder. A scale sized only for average flow may overload during a busy shift. Too much spare capacity can also reduce useful resolution. That trade-off is easy to miss.
Accuracy figures need context. OIML Recommendation R 50-1 defines belt-weigher accuracy classes of 0.2, 0.5, 1, and 2. These classes offer a benchmark, not a promise of identical results on every belt. Installation, belt tension, material distribution, and calibration all affect performance. NIST Handbook 44 provides requirements and test procedures for belt-conveyor scale systems, supporting checks under operating conditions. Ask how accuracy is verified with your material and actual belt speed.
Technology matters. A typical system combines a weigh frame, load cells, a belt-speed sensor, and an integrator. Digital diagnostics can flag signal drift or speed-sensor faults before totals look suspicious. Still, extra features do not fix poor alignment. Look for accessible calibration points and clear fault records. Then compare test results with routine production records. Real plants are messy; that detail matters.
Evaluating Conveyor Layout and Operating Conditions
A conveyor scale must fit the conveyor that actually runs, not just the layout on a drawing. Measure belt width, speed range, incline, and the distance between loading points and transfer chutes. Note where the belt vibrates or tracks unevenly. Small changes matter. A weigh span needs stable belt support, consistent tension, and enough straight running length for repeatable readings. Check whether nearby idlers, frame joints, or access platforms could affect movement or maintenance. Measure the real belt.
Operating conditions can change the measurement. Damp fines may cling to the belt, while coarse material can arrive in uneven surges. Record typical and peak flow rates, along with temperature, dust, and washdown exposure. If the conveyor starts and stops often, assess how readings behave during those transitions. A clean, steady test can be misleading. Compare performance under ordinary production conditions, not only during an easy trial. It is tempting to assume the belt stays centered and the load stays even; that assumption deserves a second look. Leave practical access for inspection and calibration, since a scale that is difficult to reach may receive less attention than it needs.
Checking Integration, Calibration, and Maintenance Needs
A conveyor scale works only as well as its connection to the line around it. Before purchase, map where its weight signal must go: a PLC, display, data historian, or control system. Confirm the signal type, communication protocol, update rate, and available I/O with the scale supplier and controls technician. A scale that measures accurately but shares data poorly can create avoidable manual checks. Small detail. Check whether belt-speed feedback comes from an encoder or another compatible source; unstable speed can distort flow readings.
Calibration needs deserve equal attention. Ask how zero and span checks are performed, what test weights or approved methods are required, and how often verification fits your operating conditions. Dust, belt tension, splice condition, and changing material loads can affect readings. Keep a record of readings, adjustments, and dates. This helps reveal drift, but records cannot fix a poor setup. That is easy to overlook.
Maintenance should match the actual site, not an idealized schedule. Check access to load cells, junction boxes, and belt-tracking points before installation. Can a technician inspect them without removing guards or stopping nearby equipment? Clarify cleaning methods and replacement-part lead times. Schedule checks after belt work or major material changes. There is a trade-off: frequent checks use labor, while long gaps may hide small faults. I would also ask who owns each task; unclear responsibility is a weakness that can be missed.


 +86-19862000127
 Phone
 Email